Blue Block Presbyopia
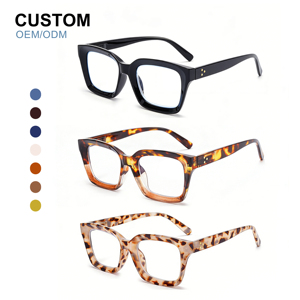
Curated wholesale silhouettes engineered with high-yield sell-through dynamics: high-definition blue-blockers, multi-axis polarized lenses, surgical memory polymers, and aerospace titanium frames.
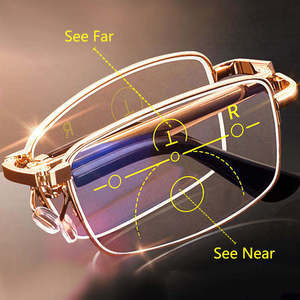
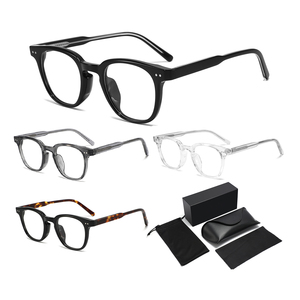
A masterclass on raw material selection, optical tolerances, CNC wire-core insertion, and regional cluster advantages across Shenzhen, Wenzhou, and Danyang.
In high-tier commercial optical markets across North America, the European Union, and Australasia, consumer demand has definitively pivoted away from excessive brand logos toward intrinsic tactile quality, structural longevity, and anatomical ergonomics. This design philosophy, commonly referred to as Quiet Luxury, presents strict challenges to original equipment manufacturers (OEM) and private-label optical brands. Eyewear is no longer treated merely as a commodity accessory; it is recognized as a medical-grade optical chassis that frames the human visage for 16 consecutive hours daily.
Achieving this level of understated elegance demands uncompromising precision throughout every industrial process: the subtle taper of a 6.0mm to 4.2mm acetate temple, micro-welded barrel hinges that open with butter-smooth hydraulic tension, and custom inner bevels calculated to eliminate optical lens stress birefringence under polarizing filters. Leading Chinese manufacturers now operate at tolerances once restricted to boutique ateliers in the Cadore valley or Sabae, Japan.
| Optical Component | Commercial Commodity Standard | Export-Grade Quiet Luxury Spec (Our Facility) | Clinical / Functional Advantage |
|---|---|---|---|
| Frontal Acetate | Recycled Extruded Scrap (<15% water content) | Cured Block Bio-Cellulose Acetate (2.8% plasticizer balance) | Eliminates post-glaze temple warping; holds manual bench adjustment indefinitely. |
| Hinge Assembly | Standard friction riveted 3-barrel zinc alloy | OBE / Comotec German 5 or 7-barrel nickel-silver with Teflon coated lock screws | Zero loosening over 25,000 opening/closing cycles; smooth, continuous tactile feedback. |
| Titanium Purity | Mixed alloy surface-plated metal wire | Grade 5 Aerospace Alpha-Beta Titanium (Ti-6Al-4V) & Pure Beta-Titanium temples | Skin biocompatibility, extreme memory elasticity, zero nickel elution under perspiration. |
| Lens Bevel Angle | Approximate 120° non-calibrated V-bevel | Exact 115° asymmetric optical V-groove (depth: 0.65mm ±0.03mm) | Prevents high-index (1.67/1.74) prescription lenses from popping out during thermal flexing. |
| Surface Finishing | Single 12-hour automated chemical polish | 72-hour multi-stage walnut shell tumbling + 3-stage manual pumice hand-buffing | Deep mirror gloss, liquid-smooth edge contours, and scratch-resistant luster. |
Procurement directors must comprehend China's distinct regional industrial topography to match specific product categories with optimal factory infrastructure:
As international regulatory frameworks tighten and consumer eco-literacy increases, global buyers are updating their procurement playbooks. The next quadrennium will be defined by three tectonic developments:
Our OEM/ODM manufacturing facilities combine Old-World artisanal bench finishing with automated optical robotics to deliver zero-defect private-label supply programs.
Every cellulose acetate and titanium front is sculpted on ultra-precise multi-axis CNC machines, maintaining a structural rim groove tolerance of ±0.03mm. This guarantees that finished lenses snap into place securely without localized stress-induced fringe distortion.
We engineer custom custom-stamped temple wire cores encased in crystal-clear acetate temples. Rather than relying on fragile glue-in or hot-pressed hinges, we utilize traditional hydraulic pin-riveting to join the hinges directly through the chassis frame.
Our high-end metal and titanium frames undergo physical vapor deposition (PVD) ion-plating within cleanroom environments. This process yields a wear-resistant metallurgical bond that withstands 96-hour continuous salt-spray and artificial sweat testing.
Mirror-grade edge finishes cannot be rushed. Frames undergo continuous 72-hour rotary tumbling through fine beechwood chips, Japanese pumice pastes, and raw walnut shells, finalized by seasoned craftsmen using carnauba wax polishing wheels.
We support growing boutique brands with comprehensive bespoke solutions: custom temple laser etching, pantone-matched acetate color casting, custom eco-leather cases, lens micro-etchings, and international compliance barcode labeling.
Every production batch is certified against mechanical fatigue, temple bridge deformation, thermal cycling stability, and dimensional integrity under ISO 12870, guaranteeing zero export roadblocks across FDA, UKCA, and CE customs zones.
Real-world insights for optical retail buyers, distributors, and brand owners seeking clarity on lead times, MOQ flexibility, lab glazing, and compliance certificates.
For in-stock catalog silhouettes (such as our high-performance TR90, photochromic sunglasses, and business titanium frames), our wholesale minimum order threshold begins as low as 12 to 50 pieces per SKU, enabling independent practices and boutique optometrists to test sell-through velocity with minimal capital exposure.
For full bespoke OEM/ODM custom manufacturing (custom pantone acetate laminations, proprietary temple tooling, unique metal hinges, and signature temple stamping), our standard MOQ is 300 pieces per frame geometry, which can be subdivided across 3 distinct colorways (100 pieces per color variant).
Yes. Every optical chassis in our portfolio is engineered strictly in accordance with ophthalmic dispensing criteria. Frames are delivered with premium demo lenses featuring laser-etched alignment datum lines. Rims are precision routed with an asymmetric 115° optical V-bevel (depth: 0.60mm to 0.68mm), specifically designed to secure single-vision, free-form digital progressives, bifocals, and high-minus indices (up to 1.74 ultra-high index resins).
Furthermore, our temple core structures feature optimized annealing zones, allowing dispensing opticians to execute manual cold or heated bench adjustments to the mastoid bend and pantoscopic tilt without risking acetate crazing.
Our manufacturing and export operations comply fully with Tier-1 international medical device and personal protective equipment standards:
Our rapid-prototyping phase delivers high-precision 3D CAD models within 48 hours, followed by CNC functional physical prototype samples within 10 to 14 working days.
Once pre-production golden samples are approved by the client, mass manufacturing cycles run according to material parameters:
Acetate warpage is caused primarily by residual internal stress and excess moisture during expedited manufacturing. To eliminate this issue, our acetate slabs undergo a specialized 45-day thermal curing seasoning phase in temperature- and humidity-controlled drying chambers prior to CNC profile milling.
For hinge stability, our assemblies incorporate imported OBE or Comotec screws treated with self-locking anaerobic micro-encapsulated polyamide patches. This engineering standard guarantees that temples resist loosening, retaining their opening resistance torque even after thousands of cycles on boutique retail display floors.